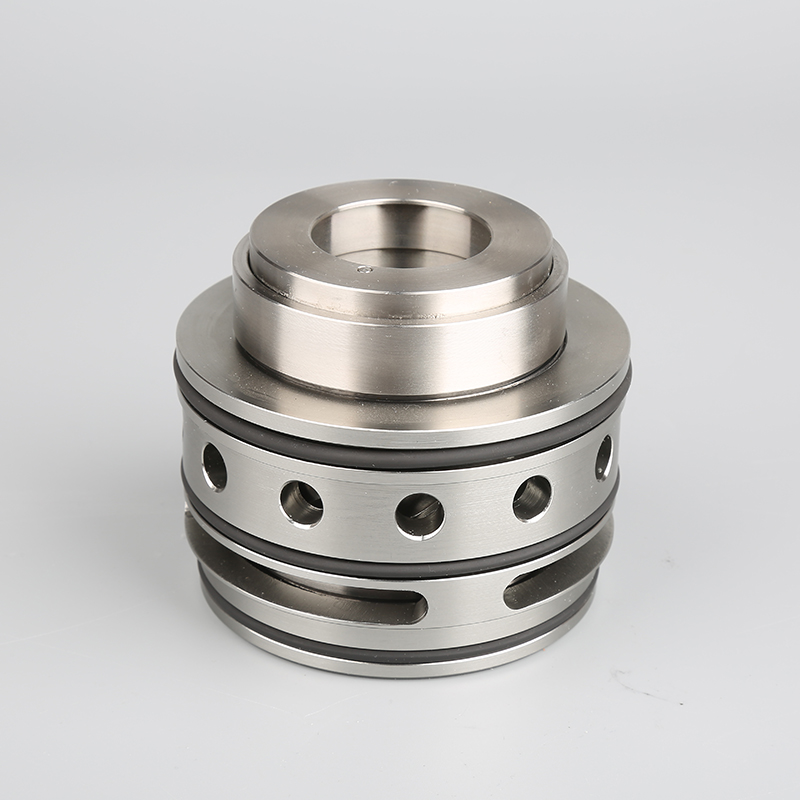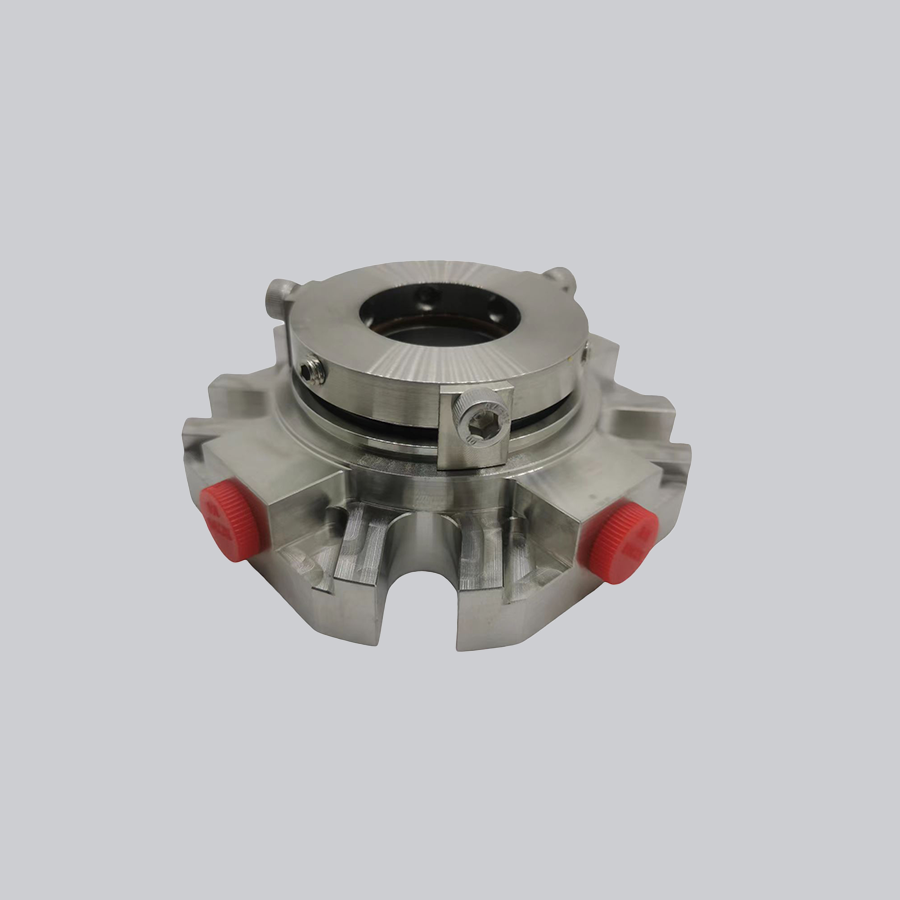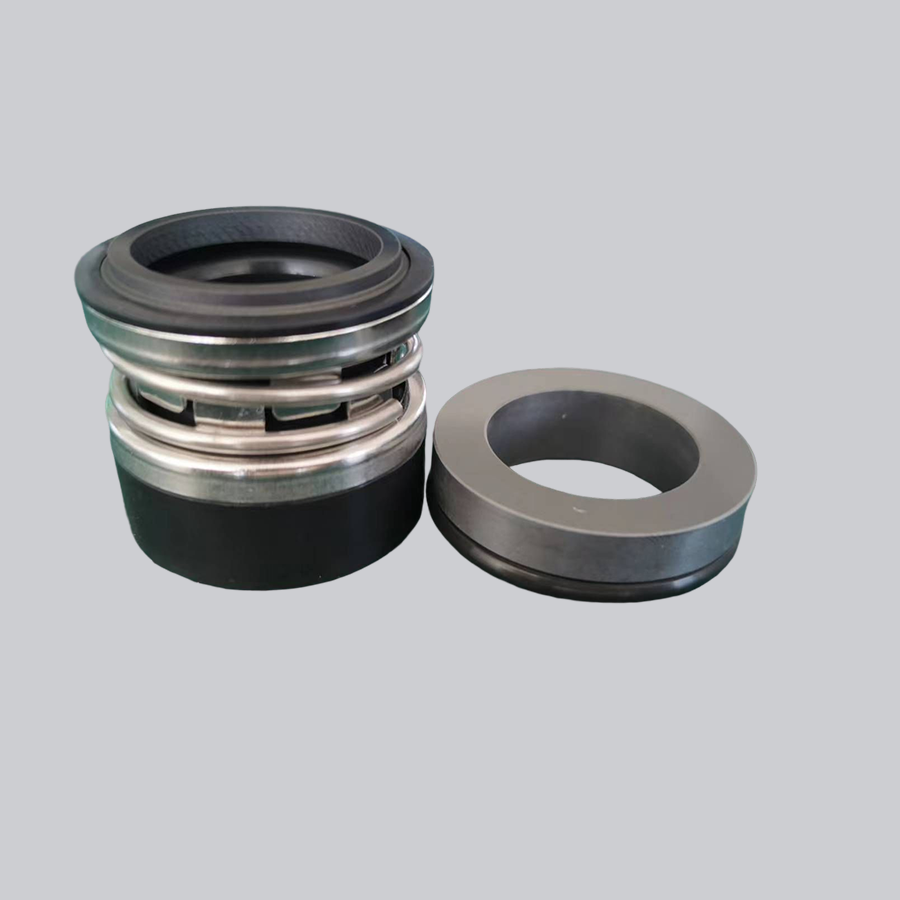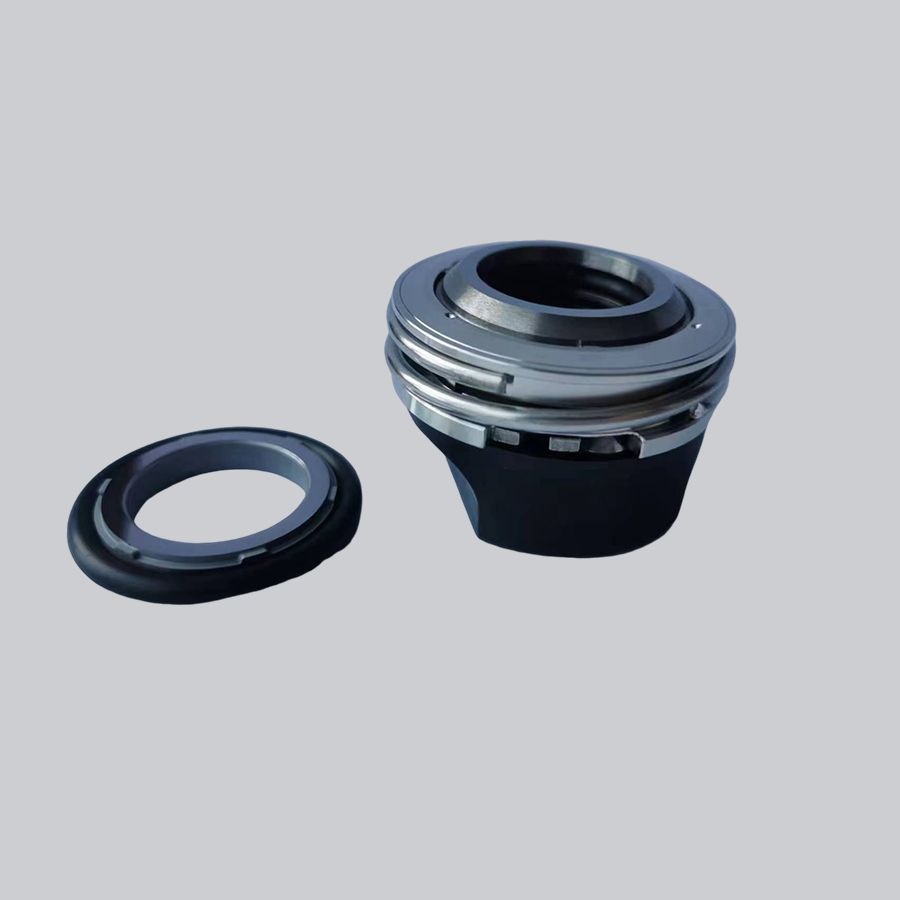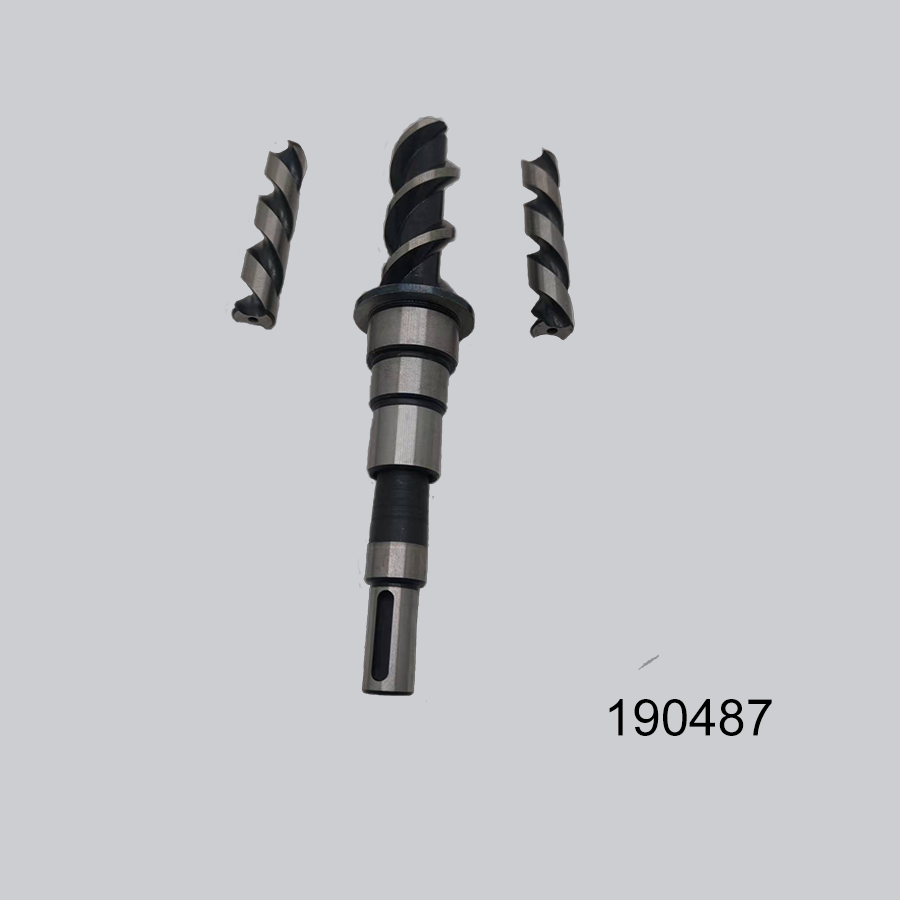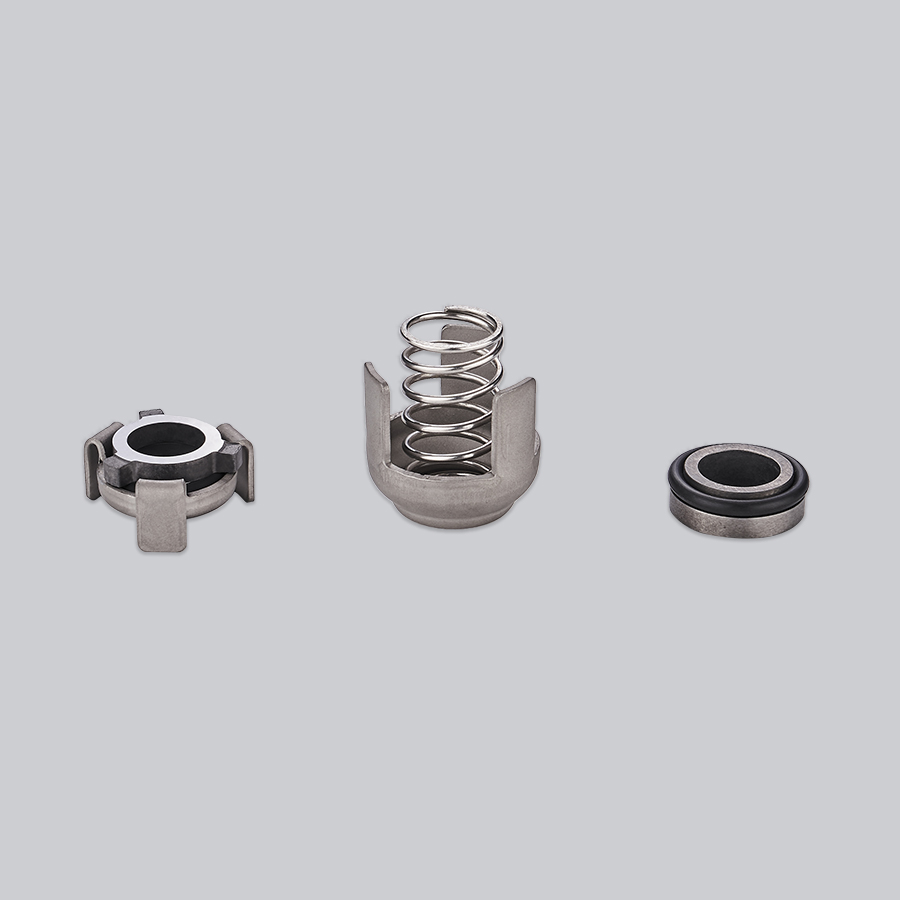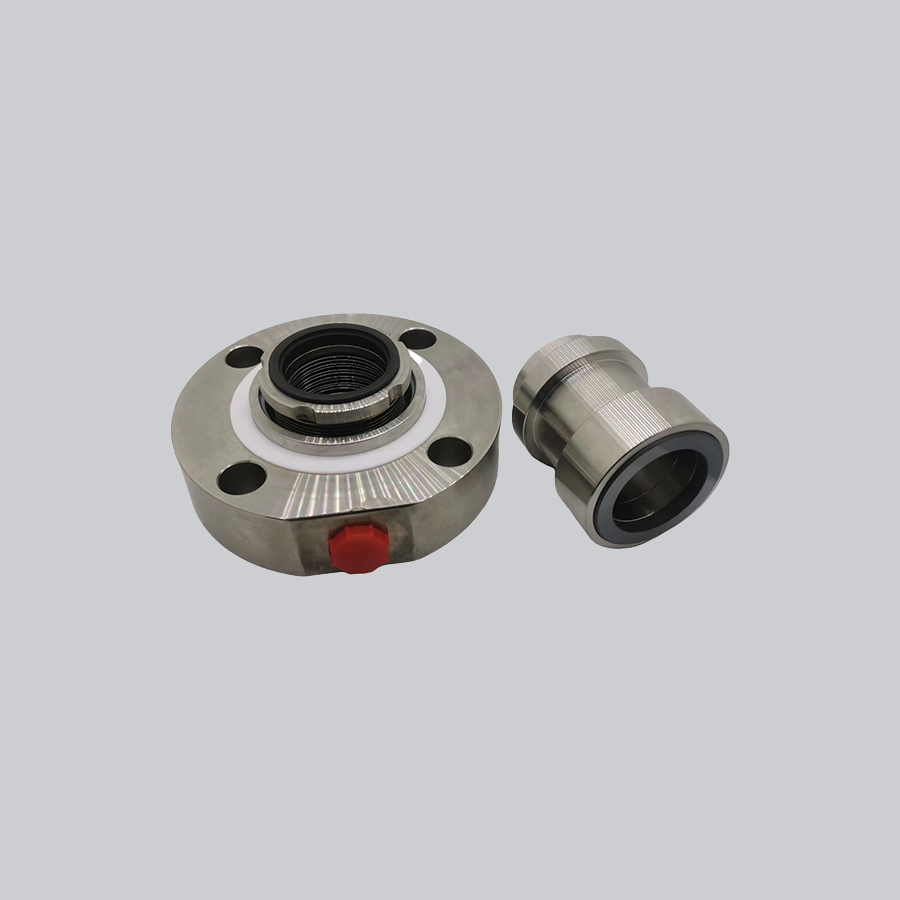


Explore our primary mechanical gland seals specially customized for high-stress chemical processing applications, pumps, and rotating equipment.
In chemical processing plants, fluid handling systems operate under rigorous conditions characterized by aggressive solvents, highly concentrated acids, abrasive crystalline slurries, and extreme thermal fluctuations. Controlling volatile emissions and preventing hazardous leakages from pump shafts, mixers, and agitation equipment is vital to workplace safety, environmental sustainability, and operational profitability.
Gland seals—comprising advanced compression packing materials and sophisticated mechanical gland cartridges—form the primary defense line against process fluid loss. Today's chemical process facilities demand sealing architectures that minimize friction coefficients, dissipate heat rapidly, and maintain dimensional stability under immense pressures.
Global environmental mandates, such as the EPA Clean Air Act and ISO 15848-1 fugitive emission standards, have compelled chemical manufacturers to transition toward zero-emission sealing systems. Mechanical gland seals engineered with dual-balanced cartridge technology and secondary containment barriers are rapidly replacing traditional packing in high-risk applications.
Selecting the right gland seal configuration requires matching material physical characteristics to specific chemical fluid behaviors.
Pumping concentrated sulfuric acid, nitric acid, and hydrofluoric acid demands chemically inert contact faces. Mechanical gland seals utilizing Reaction Bonded Silicon Carbide (RBSIC) or Sintered Silicon Carbide (SSIC) paired with synthetic carbon graphite provide unmatched corrosion resistance and wear mitigation.
Viscous resins, polymers, and synthetic latex present unique challenges due to high shearing forces and thermal buildup. Single-spring or metal bellow gland seal cartridges prevent spring clogging and maintain uniform face loading across fluctuating fluid viscosities.
In fertilizer manufacturing and mining fluid recovery, slurry particles can destroy sealing faces rapidly. Hard-on-hard seal face pairs (Tungsten Carbide vs. Tungsten Carbide) configured within flush-assisted mechanical gland housing extend operational lifespan significantly.
Modern chemical process sealing relies on state-of-the-art ceramic, metallic, and elastomeric compounds engineered to withstand localized pitting, thermal shock, and chemical degradation. At Ningbo Victor Seals Co., Ltd, our product lines utilize top-grade raw materials tailored to specific chemical media environments.
Key materials include pure graphite rings, pressure-sintered silicon carbide, premium tungsten carbide alloys, and perfluoroelastomer (FFKM) secondary static seals capable of resisting continuous temperatures exceeding 300°C.
The integration of IoT diagnostics into chemical gland sealing boxes represents a major paradigm shift. Embedded sensors continuously monitor barrier fluid pressure, barrier fluid temperature, vibration levels, and micro-leakage rates in real-time, feeding diagnostic telemetry to central control systems.
This predictive maintenance capability minimizes unplanned catastrophic pump failures, optimizes maintenance cycles, and safeguards plant personnel from unexpected toxic fluid releases.
Ningbo Victor Seals Co., Ltd was founded in 1998, more than 20 years ago, and is strategically located in Ningbo, Zhejiang province, China. Our modern manufacturing facility covers a total land area of 3,800 square meters with a construction footprint of 3,000 square meters. We employ a dedicated team of over 40 highly skilled professionals, establishing our position as a premier mechanical seals manufacturer in China.
Our flagship brand "victor" is internationally recognized and registered in more than 30 countries worldwide. We specialize in producing complete sets of mechanical seals, including cartridge seals, rubber bellow seals, metal bellow seals, and o-ring seals engineered for demanding operating conditions.
Additionally, we provide tailored OEM mechanical seals designed specifically for unique working parameters according to client specifications. We manufacture high-precision spare parts using elite materials such as Silicon Carbide, Tungsten Carbide, Ceramic, and Carbon for seal rings, bushings, and thrust discs.
All products are rigorously designed in alignment with international standard specifications including DIN24960, EN12756, ISO3069, API610, API682, and GB6556-94. Our products are extensively deployed across petroleum, chemical processing, power generation, machinery, metallurgy, shipbuilding, sewage treatment, printing and dyeing, food processing, pharmaceuticals, and automotive industries.
Full-lifecycle support ensuring maximum reliability for your critical fluid handling assets.
Over two decades of specialized engineering experience in mechanical seal design, fluid dynamics, and material development.
Direct factory pricing offering up to 10% lower cost compared to other international top-tier suppliers without compromising quality.
Equipped with state-of-the-art CNC machining, ultrasonic testing, and optical lapping machines ensuring precision execution.
100% rigorous pressure testing, dimensional verification, and material certification for every piece before shipment.
Massive ready-to-ship stock for standard mechanical seals, minimizing plant downtime during emergency replacements.
Streamlined order dispatch via international air express (DHL, TNT, FedEx, UPS) and ocean freight lines.
Our chemical process sealing solutions operate seamlessly across critical industrial sectors.

Select high-performance gland seals and replacement assemblies for chemical, industrial, and marine pump equipment.