

Engineered for high reliability, maximum corrosion resistance, and operational efficiency in demanding fluid handling applications.
Navigating harsh environments, aggressive media, and stringent environmental regulations with advanced mechanical seal technology.
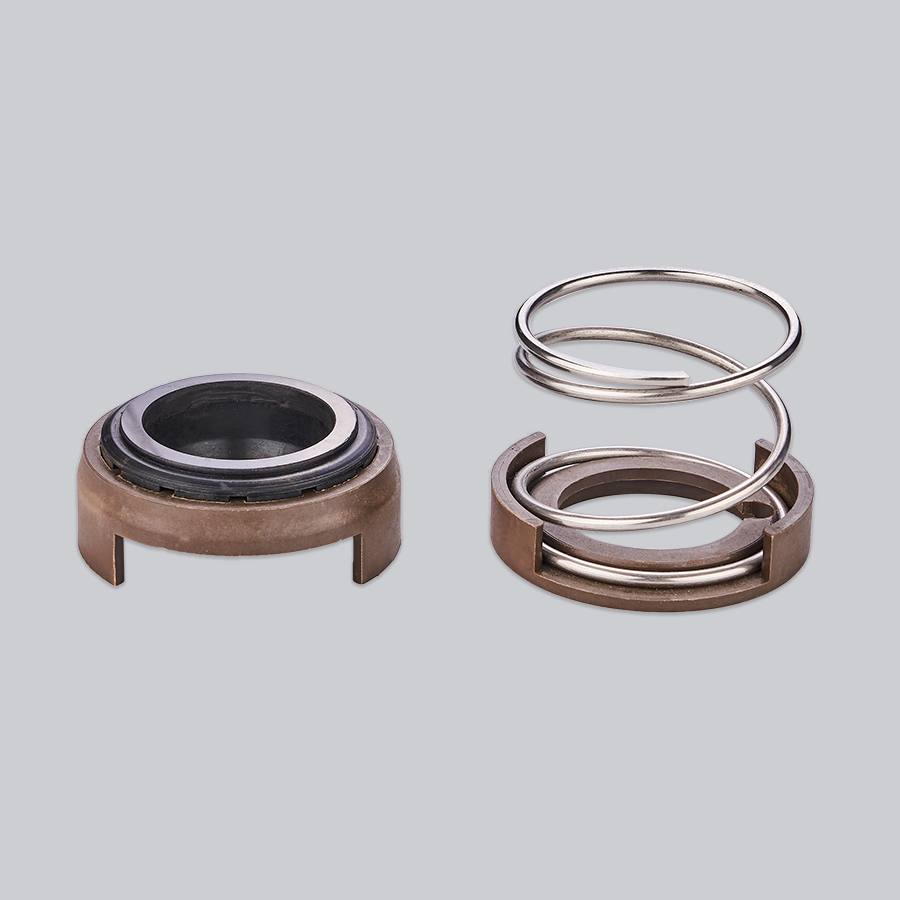
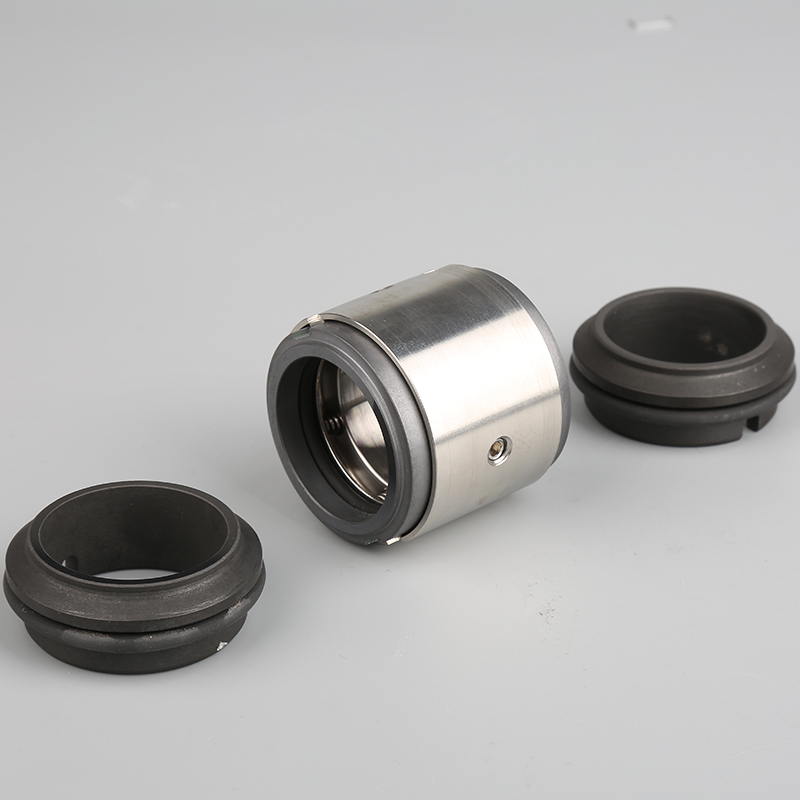
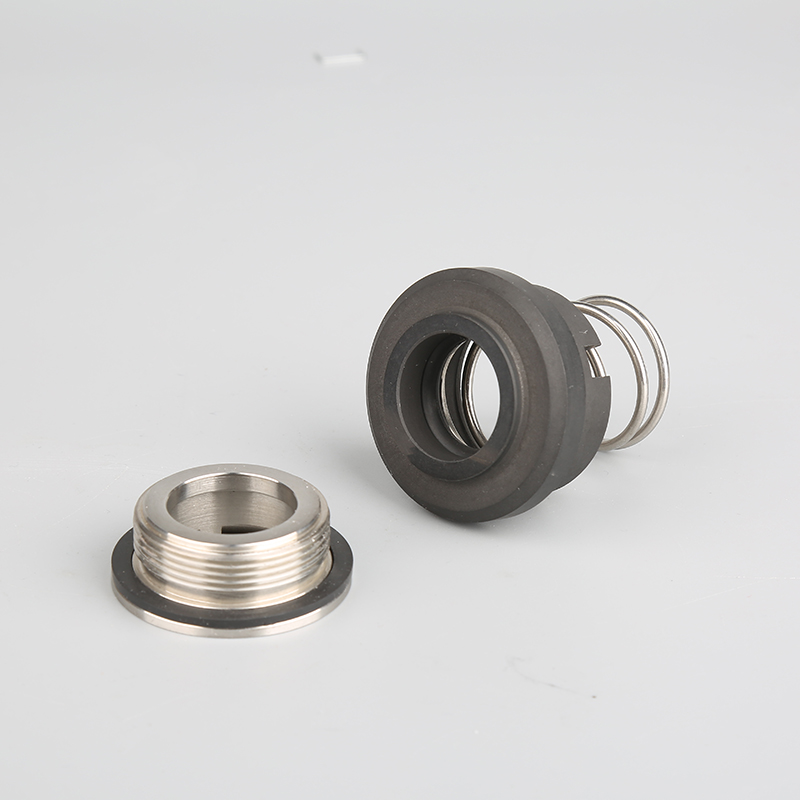
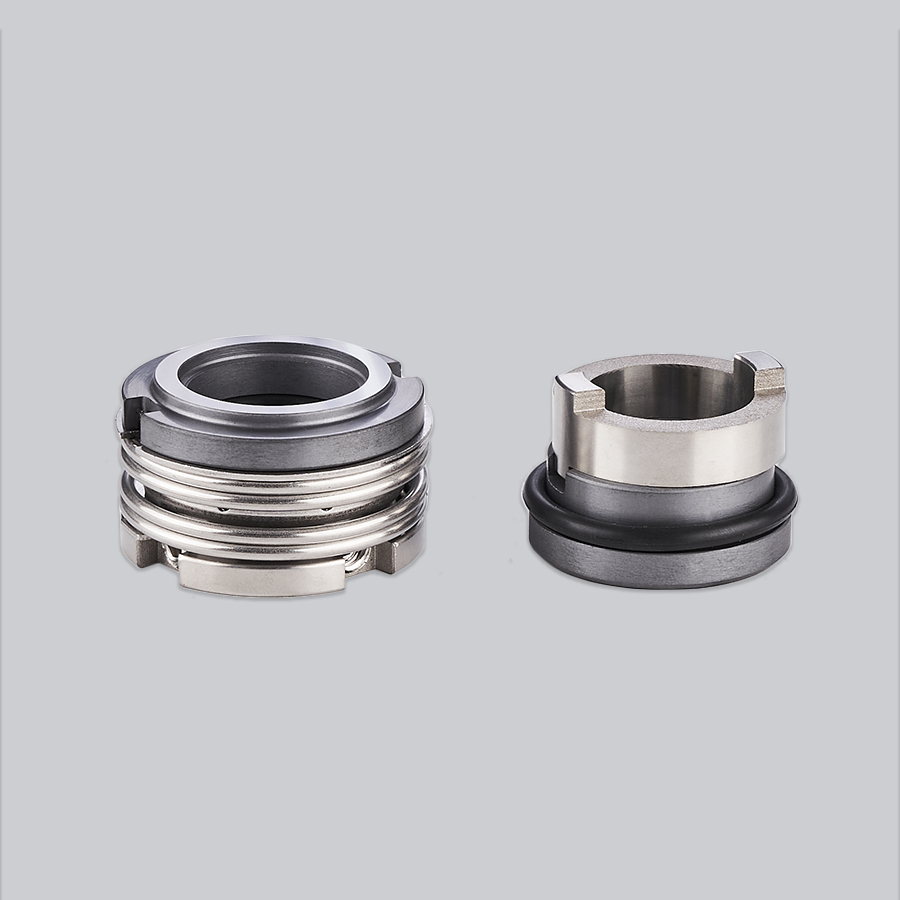
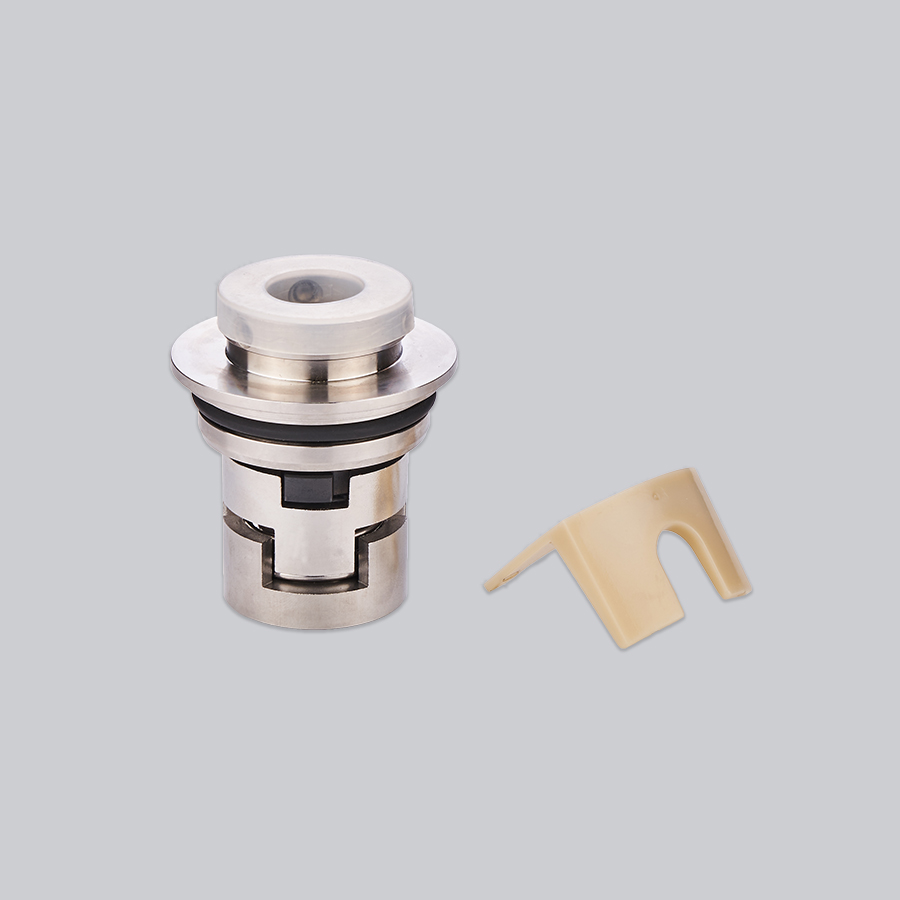
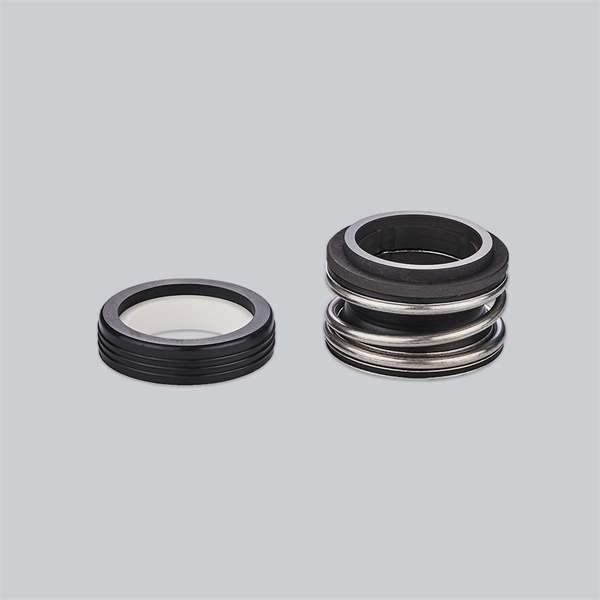
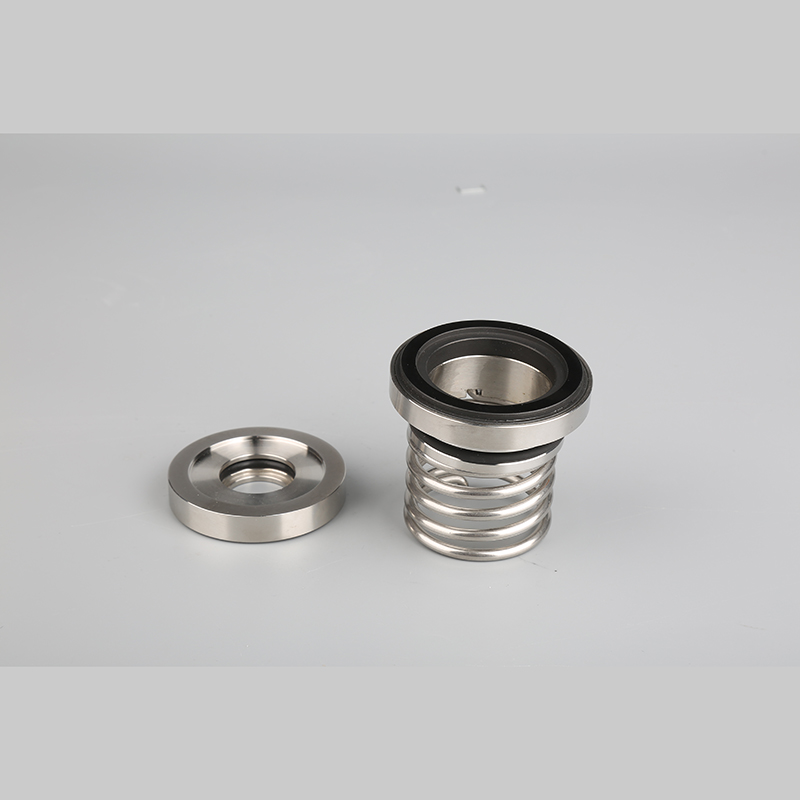
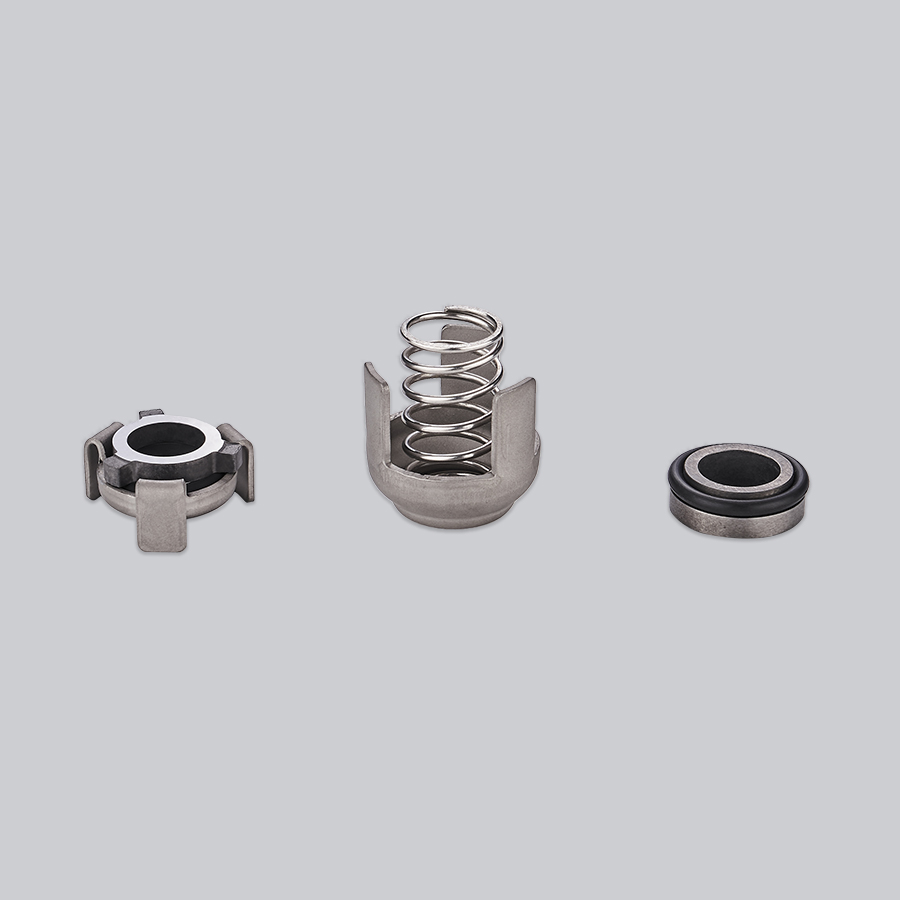
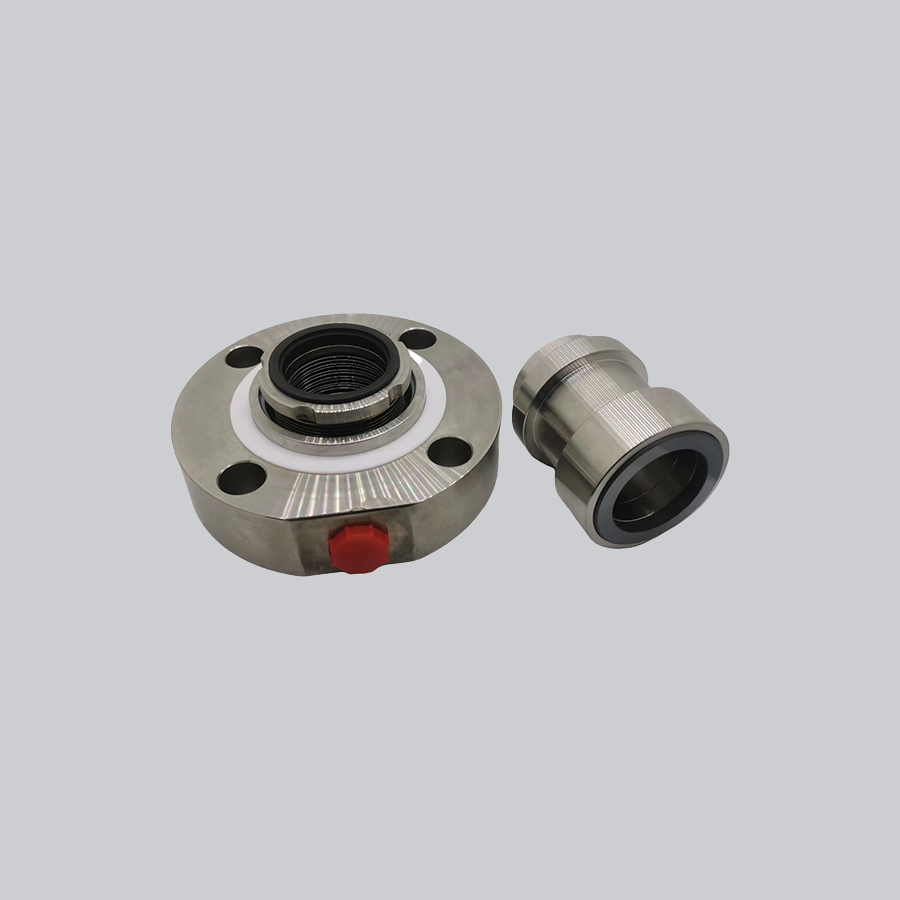
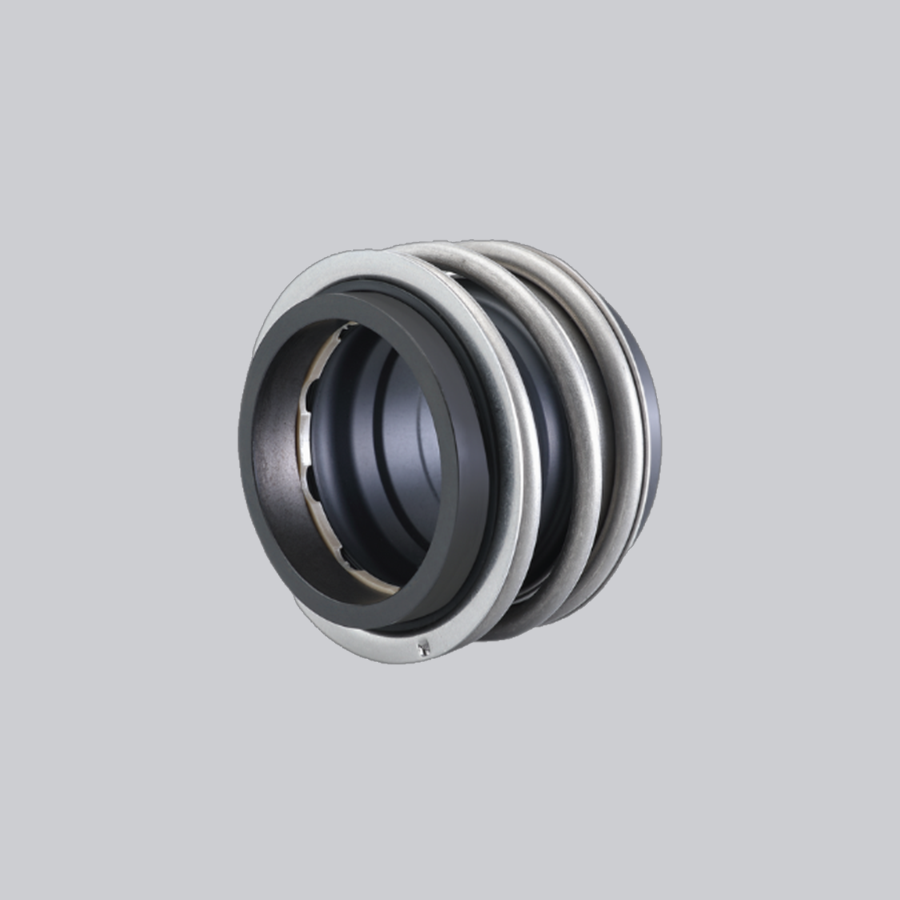
In modern chemical processing plants, fluid isolation and leak prevention are fundamental to operational safety, environmental compliance, and profitability. Fluid handling equipment operates continuously under aggressive conditions, involving highly corrosive acids, volatile organic compounds (VOCs), abrasive crystallizing slurries, and elevated operating temperatures. Among the various pumping technologies utilized across the sector, submersible pumps, mixers, and agitators rely heavily on specialized mechanical sealing architectures. Applying an optimized Flygt Seal For Chemical Process Sealing provides the robust barrier needed to withstand these aggressive fluids while preventing catastrophic equipment failures.
Originally designed for heavy-duty submersible wastewater management, Flygt pump seal designs have evolved dramatically into versatile, heavy-duty mechanical seal platforms adopted across chemical manufacturing, petrochemical processing, and hazardous effluent management. Chemical plants often process aggressive fluids such as hydrochloric acid, sulfuric acid, sodium hydroxide, and solvents. Standard pump packing or entry-level mechanical seals frequently fail prematurely when exposed to such harsh media, causing costly downtime, severe environmental contamination, and worker safety risks. High-performance mechanical seals engineered specifically for Flygt equipment bridge the gap between heavy industrial durability and chemical-grade material compatibility.
Designed to satisfy modern LDAR (Leak Detection and Repair) and EPA guidelines, ensuring hazardous chemical vapors and toxic liquids remain completely contained.
Utilizing high-grade Silicon Carbide (SiC), Tungsten Carbide (TC), and specialized elastomers like FFKM and Viton to handle aggressive acids and caustics.
Incorporating independent upper and lower mechanical seal arrangements to create a fail-safe oil or barrier chamber, shielding the motor core from fluid ingress.
The operational demands placed on a Flygt Seal For Chemical Process Sealing vary considerably depending on the chemical process stage and fluid composition. Below is an in-depth evaluation of primary industrial applications where customized Flygt mechanical seals deliver exceptional reliability:
The global industrial seal market is experiencing a significant shift driven by industrial automation, sustainability mandates, and predictive maintenance technologies. Understanding these commercial trends helps chemical plant engineers select future-proof sealing solutions:
1. Shift Toward Plug-In and Cartridge Designs: Traditional component seals require meticulous manual alignment during installation, leaving room for human error that leads to premature face misalignment. The industry is rapidly adopting cartridge and pre-assembled plug-in Flygt replacement seals. These unitized modules allow fast, error-free installation, drastically reducing Mean Time Between Failures (MTBF) and minimizing plant shutdown times.
2. Integration of Smart Monitoring & AI Diagnostics: Modern chemical facilities are integrating Smart Internet of Things (IoT) sensors directly into pump seal barrier fluid loops and oil chambers. Real-time tracking of barrier pressure, temperature, and moisture intrusion allows predictive maintenance algorithms to flag seal face wear before catastrophic fluid failure occurs.
3. Advanced Material Sciences & Surface Coatings: The development of diamond-like carbon (DLC) face coatings and nanostructure ceramic composites has expanded the operating limits of mechanical seals. These advanced materials reduce friction coefficients by up to 50%, enabling seals to withstand temporary dry-running conditions during pump priming or batch fluid changeovers.
Years Experience
Factory Area
Global Brand Registrations
Cost Advantage
Ningbo Victor Seals Co., Ltd – A Trusted Global Manufacturer of Precision Mechanical Sealing Systems
Ningbo Victor Seals Co., Ltd was founded in 1998, more than 20 years ago, located in Ningbo, Zhejiang province, China. Our modern manufacturing facility covers an area of 3800 square meters with a total construction area of 3000 square meters, employing more than 40 highly skilled professionals. We are recognized globally as a leading, highly professional mechanical seal manufacturer specializing in chemical process seals, OEM replacements, and custom fluid containment systems.
Our flagship brand "Victor" has been officially registered in more than 30 countries worldwide. Our extensive product portfolio encompasses complete mechanical seal assemblies, including cartridge seals, rubber bellow seals, metal bellow seals, and o-ring seals, designed for diverse, demanding working conditions. In addition, we provide customized OEM mechanical seals tailormade for unique operational conditions according to exact customer specifications and engineering drawings.
To ensure maximum resistance to wear and chemical attack, we manufacture high-precision spare parts using premium materials including Silicon Carbide, Tungsten Carbide, Ceramic, and Carbon for seal rings, shaft bushings, and thrust discs. All our seal products are engineered and produced in strict compliance with international industrial standards, including DIN24960, EN12756, ISO3069, API610, API682, and GB6556-94. Today, our products are widely deployed across petroleum refining, chemical processing, power plants, heavy machinery, metallurgy, shipbuilding, sewage treatment, textile printing and dyeing, food and beverage processing, pharmaceuticals, automotive industries, and more.
Delivering unmatched reliability, economic value, and engineering excellence to chemical process operators globally.
Over two decades of deep practical engineering knowledge in mechanical seals design and chemical application troubleshooting.
Direct manufacturer pricing supplying premium quality at roughly 10% lower cost than competing suppliers.
State-of-the-art CNC machining, lapping, testing rigs, and precision inspection tools ensure microscopic face flatness.
Rigorous quality management system with 100% inspection of critical dimensions and pressure testing prior to dispatch.
Large inventory reserves for standard mechanical seal lines ensuring instant dispatch for urgent breakdown maintenance.
Streamlined logistics partnerships ensuring fast air and sea delivery to minimize downtime for international clients.
Our engineered mechanical seal solutions serve critical fluid handling equipment across diverse global sectors.
Clear answers to common questions regarding ordering, technical support, material options, and customization.
For stock items, we can ship them immediately after payment is received. For non-stock items, we require approximately 15-20 days for mass production.
We are a direct manufacturing factory located in Ningbo, Zhejiang, China.
Our factory is located in Ningbo, Zhejiang Province, conveniently situated near major international shipping ports.
Yes, of course. We can offer free samples for customers to check quality before full production, with freight collect.
We usually ship goods via express carriers like DHL, TNT, FedEx, and UPS. We can also arrange air freight and sea freight based on customer requirements.
We accept T/T (Telegraphic Transfer) payment before qualified goods are ready for shipment.
Yes, customized products and OEM solutions are fully available upon request.
Yes! Our engineering team can develop the optimal seal design based on your specific application details and working conditions.
Explore our wide selection of industrial replacement mechanical seals and rotary equipment spare parts.