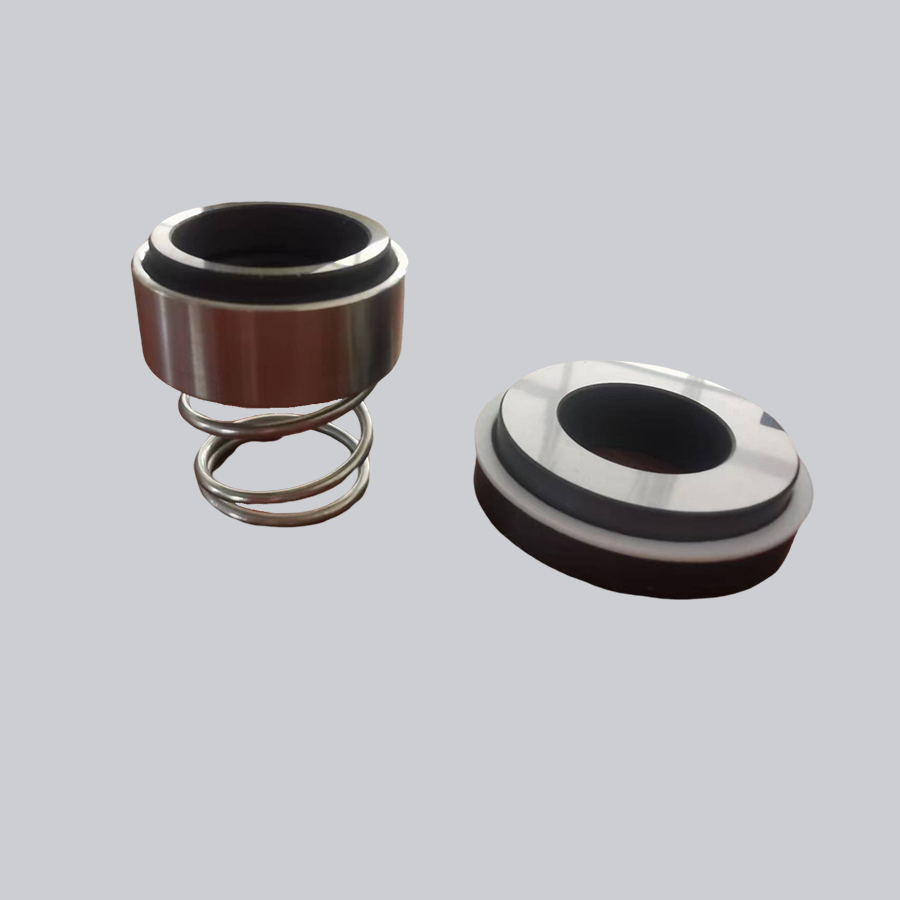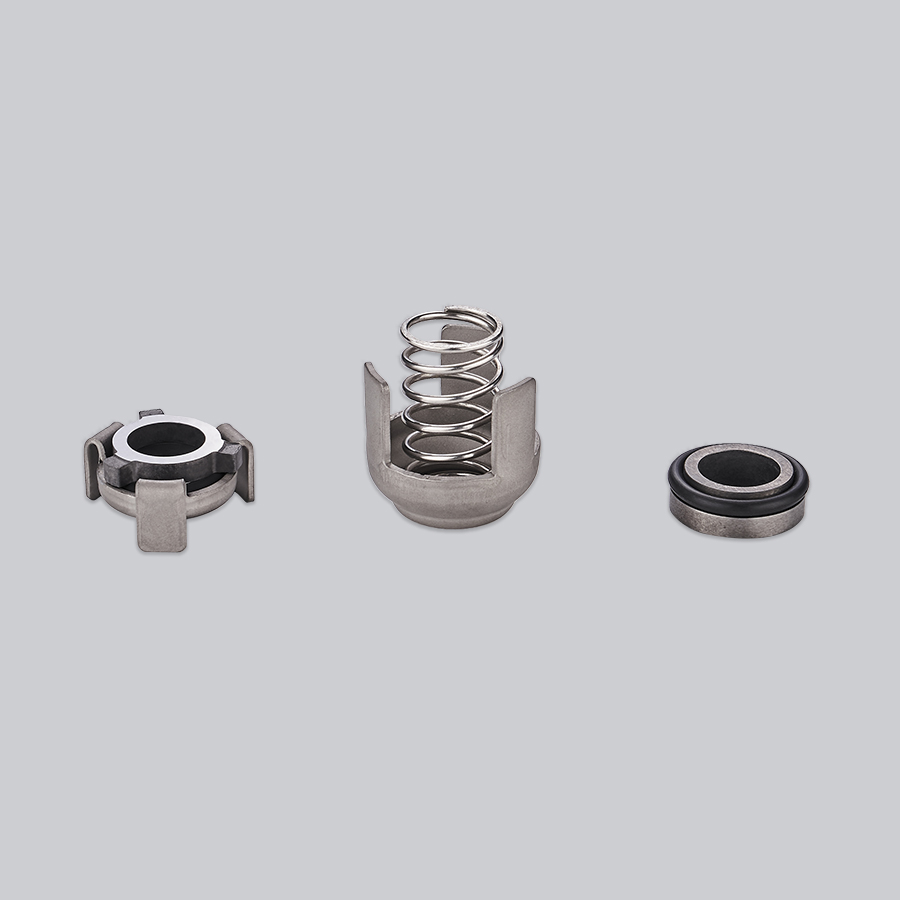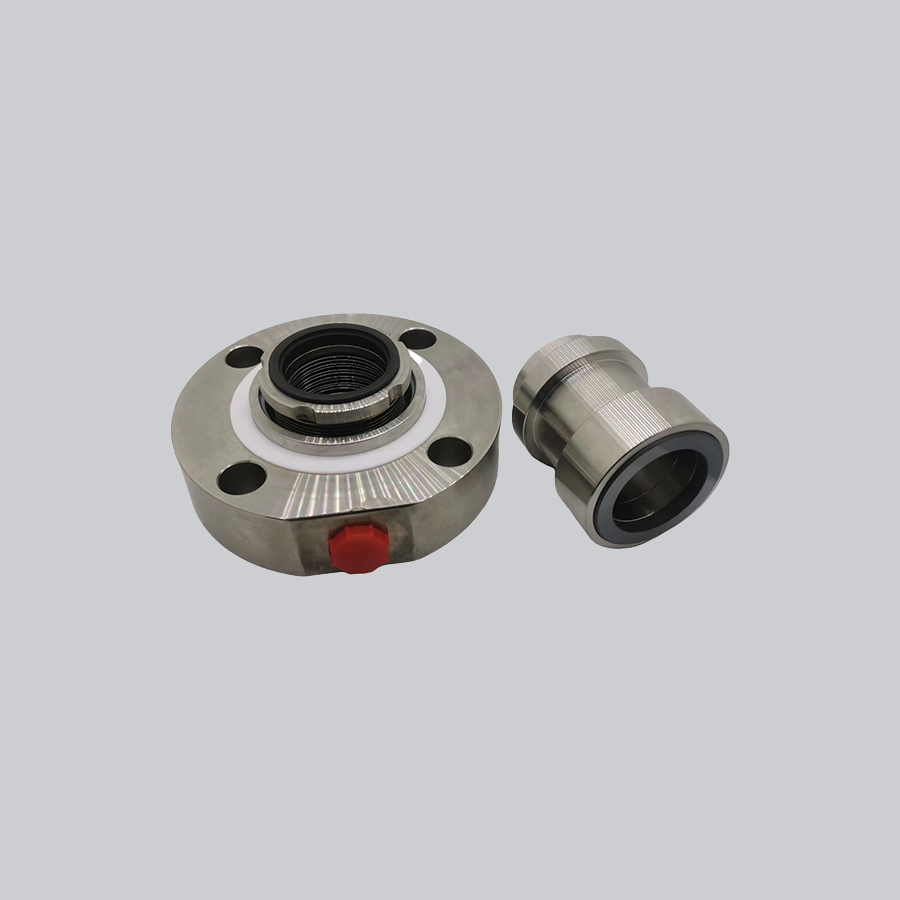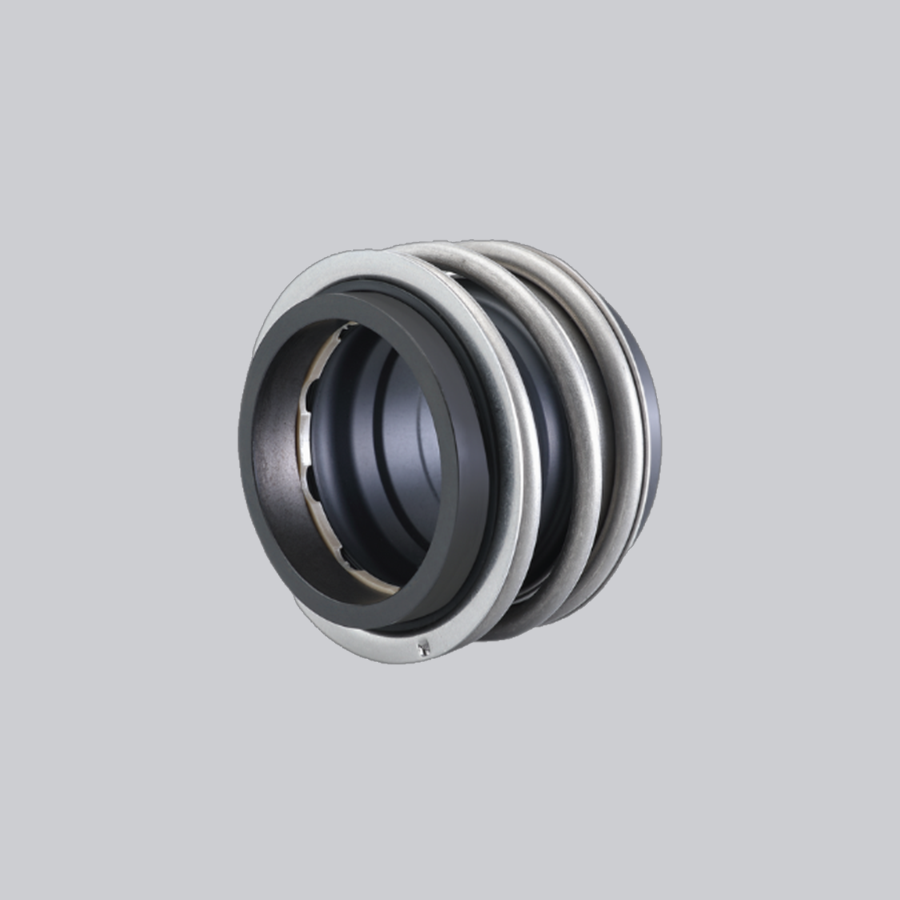


In modern industrial fluid dynamics, the performance and operational longevity of pumping machinery depend heavily on the integrity of the shaft sealing interface. An oil ring seal for pump shaft sealing serves as an indispensable engineering component designed to prevent fluid leakage, suppress wear on rotating elements, maintain optimal barrier pressure, and protect internal bearing assemblies against hazardous environmental contamination. As global industrial processes move toward higher operational pressures, elevated thermal ranges, and stringent environmental sustainability regulations, selecting the optimal oil ring seal and mechanical seal configuration is critical to preventing unscheduled downtime and expensive fluid loss.
The global industrial seal market is undergoing a rapid evolution driven by smart manufacturing trends, strict environmental regulations (such as zero-leakage mandates), and the demand for energy-efficient rotating equipment. According to recent market intelligence reports, the mechanical seal and oil ring seal industry is expanding significantly, driven by growth in water treatment infrastructure, offshore oil and gas production, chemical refining, and mining operations worldwide.
Plant operators are increasingly transitioning from traditional packing materials to precision engineered oil ring seal for pump shaft sealing systems. Modern pump systems demand seals capable of dry-running resilience, self-lubricating face dynamics, and extreme thermal tolerance. In addition, OEM pump maintenance teams prefer standard-compliant drop-in replacements—such as those replacing Vulcan, Burgmann, Grundfos, Allweiler, and IMO pump seals—to reduce maintenance lead times and operational overhead.
The fundamental mechanism of an oil ring seal for pump shaft sealing relies on maintaining a controlled hydrodynamic fluid film between rotating and stationary sealing faces. The primary oil ring acts as a dynamic barrier, while elastomer secondary seals (O-rings, bellows, or V-rings) seal static leak paths along the shaft sleeve and housing gland.
Selecting the right materials for face pairs and secondary oil rings is decisive for ensuring longevity in aggressive process media:
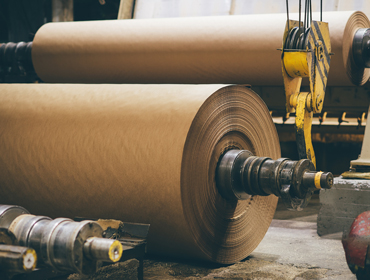
In pulping and paper bleaching lines, pumps transport fibrous slurries and aggressive chemicals. Our chemical-resistant oil ring seals prevent fiber clog and shaft wear.
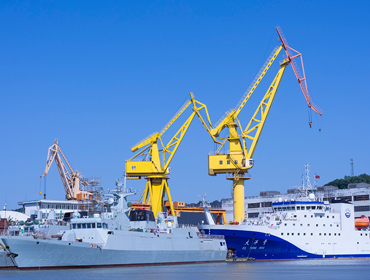
Marine engine rooms rely on heavy-duty fuel oil transfer, ballast, and bilge pumps. OEM replacements for IMO and Allweiler pumps ensure continuous marine operation.
Submersible sewage pumps and municipal water booster pumps require robust O-ring pusher seals and rubber bellow mechanical seals for zero leakage performance.
Handling solvents, acids, and volatile organic compounds requires cartridge seals with specialized elastomer O-rings compliant with DIN24960 and API682 standards.
Heavy slurry pumping applications demand high-hardness Silicon Carbide and Tungsten Carbide faces paired with reinforced shaft oil rings to handle high solids content.

Upstream drilling, midstream pipeline pumps, and downstream refineries demand metal bellow and balanced mechanical cartridge seals to ensure explosive gas containment.
Ningbo Victor Seals Co., Ltd was founded in 1998, more than 20 years ago, located in Ningbo, Zhejiang province. Our modern manufacturing factory covers an area of 3800 square meters with a construction area of 3000 square meters, employing more than 40 highly skilled employees. We stand as a leading, professional mechanical seal manufacturer and engineering solution provider in China.
Our trademark brand "victor" has been successfully registered in more than 30 countries worldwide. Our extensive main product lineup includes complete sets of mechanical seals—such as cartridge seals, rubber bellow seals, metal bellow seals, and O-ring seals—specifically dynamic engineered for diverse demanding working conditions.
Simultaneously, we specialize in offering high-precision OEM mechanical seals tailored for custom working conditions according to exact client specifications. Our internal machining and powder metallurgy divisions manufacture premium component spare parts utilizing advanced materials, including Silicon Carbide, Tungsten Carbide, Ceramic, and Carbon for seal rings, bushings, and thrust discs. All products are manufactured in strict compliance with DIN24960, EN12756, ISO3069, API610, API682, and GB6556-94 international standards.
Direct drop-in replacements for major global pump seal brands including Burgmann, Vulcan, Grundfos, Flygt, IMO, and Allweiler with 100% dimensional precision.
Comprehensive refurbishment, re-facing, and seal reconditioning services for complex industrial cartridge seals, extending equipment operating lifespans.
Dedicated engineering team providing rapid prototyping, material customization, and 3D modeling tailored to non-standard pump shaft sealing environments.
Every mechanical seal and oil ring assembly undergoes rigorous pressure testing, dimensional verification, and optical flatness inspection before dispatch.
24/7 technical hotline, installation assistance, and rapid response team dedicated to resolving operational pump sealing issues promptly.
Maintained buffer inventory for standard mechanical seal lines ensures fast lead times and instant emergency shipping via express air or sea freight.
Over two decades of continuous innovation and engineering mastery in mechanical shaft seal manufacturing and failure analysis.
Direct manufacturer pricing structure delivering high precision seals at a minimum 10% lower cost compared to traditional market suppliers.
State-of-the-art CNC machining centers, automated lapping machines, vacuum sintering furnaces, and laser measuring systems.
Zero-defect quality policy utilizing premium raw materials and rigorous ISO 9001 compliant manufacturing workflows.
Comprehensive inventory of standard sizes for Grundfos, Flygt, IMO, and Allweiler pump replacements available for instant dispatch.
Established international shipping channels ensuring safe and expedited door-to-door delivery across North America, Europe, Asia, and the Middle East.
Proper installation and preventative maintenance are essential to achieving optimal service life from your oil ring seal for pump shaft sealing systems. Improper alignment or clean room violations during installation account for over 60% of premature mechanical seal failures.
For stock items, we ship immediately after receiving payment. For customized or non-stock mass production items, our typical lead time is 15 to 20 days.
We are a direct manufacturing factory located in Ningbo, Zhejiang, China, with complete in-house machining, lapping, and assembly facilities.
Our facility is situated in Ningbo, Zhejiang province. We welcome international customers and audit teams to visit our production facility.
Yes, we provide free evaluation samples for standard items so customers can verify material quality and dimensional fit prior to mass production (freight collect).
We ship globally via express carriers like DHL, TNT, FedEx, and UPS. Large volume orders are dispatched via air or ocean container freight based on customer preference.
We accept T/T (Telegraphic Transfer) prior to dispatch of qualified finished goods. Flexible terms can be arranged for long-term partners.
Yes! Custom engineered mechanical seals and non-standard oil ring seals are one of our core specialties. We fabricate according to your specs.
Absolutely. Our engineering team can reverse engineer drawings from your worn physical samples or pump housing measurements to deliver an optimized design.